01
Review
Process, hazards and existing documents are reviewed.

WETS AI engineers and builds control panels for chemical plants from our Houston, Texas shop. We design batch, dosing and continuous process controls with input from HAZOP and SIL identification, build each panel to UL 508A, and prove every sequence and interlock before it ships.
Chemical processes leave little room for a control system that does something unexpected. Sequences must run in the right order, ingredients must be added in the right amounts, and the plant must reach a safe state when something goes wrong.

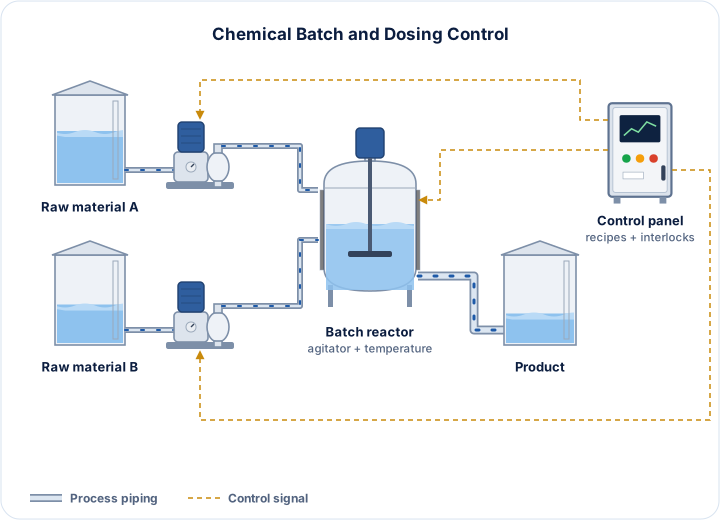
The panel runs each recipe step by step, metering raw materials into the reactor and holding temperature until the batch is ready.
Our engineers take part in HAZOP reviews and carry out SIL identification, so the safeguards agreed in those studies are carried directly into the drawings, the program and the test procedure.
Safety functions are kept separate from normal process control, and every trip is tested at FAT and again on site at SAT. See design and engineering for how this works.

Chemical plants often have areas classified for flammable gases or vapors. Our UL 508A panels are built for general-purpose (unclassified) locations such as control rooms and MCC rooms, with field wiring running out to the process.
Tell us the area classification at the start, so the panel location, field devices and wiring are planned correctly from the first drawing.
Process, hazards and existing documents are reviewed.
Sequences, interlocks and alarms are agreed in writing.
Panel and program are built from the same narrative.
Every sequence and trip is tested at FAT and SAT.
Yes. Our engineers take part in HAZOP reviews and carry out SIL identification, and the results feed directly into the panel design and testing.
Yes. We build batch reactor and dosing controls, with recipes and sequences agreed in the control narrative.
Our UL 508A panels are built for installation in general-purpose (unclassified) locations, such as control rooms, MCC rooms and outdoor areas outside the classified zone. Tell us the area classification early so the panel location and field wiring are planned correctly.
Allen-Bradley, Siemens and Schneider Electric, matching your plant standard.
About 16 weeks on average from order to shipment. The real figure depends on panel size and on component lead times, so we confirm a schedule with every quotation.
Control narratives, HAZOP and SIL identification, process flow diagrams and panel drawings.
Programs written in-house for Allen-Bradley, Siemens and Schneider Electric, tested at FAT.
The 13 checks every panel passes, plus witnessed FAT and SAT on site.
Share your process description or P&IDs. We will review them with you and quote the engineering and the panel.